

Industrial Chemical
Monitor the health and performance of your machines in the chemical industry
In the chemical industry, the continuity of production, access constraints in hazardous environments, and strict environmental safety requirements make the monitoring of electrical machines more complex.
Operational constraints
Secure and optimize your operations
The slightest unexpected failure leads to colossal financial losses: loss of production batches, disruption of chemical reactions, and the risk of toxic waste. Ensuring zero unplanned downtime is vital.
Process security
The interruption of an ongoing chemical reaction or the interruption of a continuous process results in the loss and disposal of the batch as well as the cleaning of the equipment.
ATEX and corrosive environments
Your equipment is immersed in toxic or acidic atmospheres. Installing physical sensors there is complex; intervening manually is dangerous.

Security
Your machines operate with flammable and pressurized fluids; anticipating deviations helps to avoid incidents that are dangerous to personnel and the environment.
Optimization of energy costs
The synthesis, separation and ventilation processes consume enormous amounts of electricity. Optimizing the consumption of your motors is vital.
RED in the chemical industry
Surveillance designed to meet your specific site constraints
RED deploys the measure in the electrical cabinet and monitors the entire machine from a single point, to facilitate the monitoring of scattered, exposed or heavily loaded equipment.
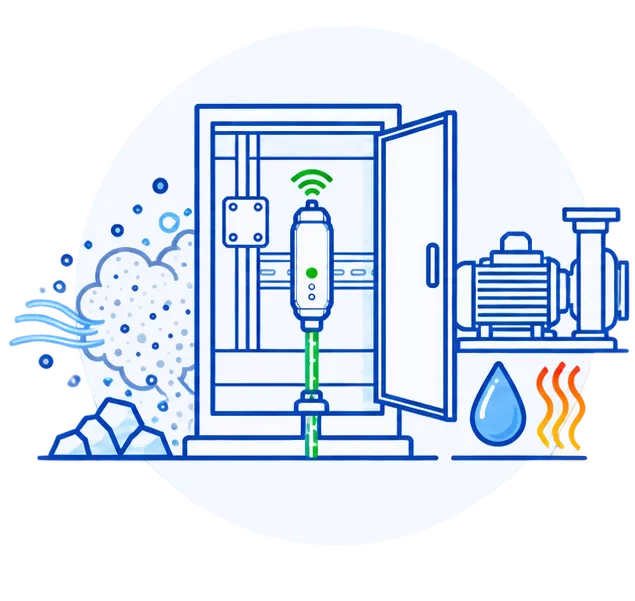
Severe off-field sensor
The RED is installed in the electrical cabinet, away from the production area and protected from dust, shocks, and other hazards.

Only one sensor per machine
A single measurement point to monitor the engine and the load it drives, minimizing instrumentation for an extended fleet.
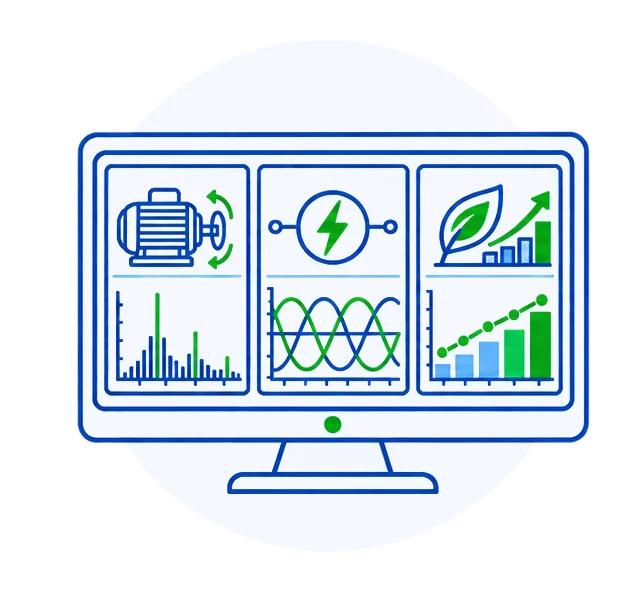
Mechanical, electrical and energy vision
RED combines these 3 types of data to provide a more comprehensive and reliable reading of the health and performance of the equipment.
AT EVERY STEP OF THE PROCESS
What equipment can you monitor with RED?
Extraction, grinding, transport, ventilation, drying or kneading: RED covers the rotating equipment essential for the continuity of your operations.
They feed your chemical reactions under pressure, liquefy the gases or distribute the control air for your valves. Far from the risk zones, we detect:
Mechanical balancers
Problems with anchoring
Discharges from hydraulic loading or operation
Degradation or wear of the lobes
Wear of the couplings
Electrical defects and abnormal changes in consumption



Use case
Some concrete cases...
Anticipate failures and secure your production
Continued monitoring to prevent critical outages and optimize energy performance.