
Chemical industry
Monitor the health and performance of your machines in the chemical industry
In the chemical industry, production continuity, access restrictions in hazardous environments and strict environmental safety requirements make the monitoring of electrical machines more complex.
Operational constraints
Secure and optimize your operations
Process safety
The interruption of a chemical reaction in progress or of a continuous process results in the loss and scrapping of the batch, as well as cleaning of the equipment.
ATEX and corrosive environments
Your equipment sits in toxic or acidic atmospheres. Installing physical sensors there is complex; intervening manually is dangerous.

Safety
Your machines work with flammable fluids under pressure; anticipating deviations helps avoid incidents that endanger personnel and the environment.
Energy cost optimization
The synthesis, separation and ventilation processes consume enormous amounts of electricity. Optimizing the consumption of your motors is vital.
RED in the chemical industry
Monitoring designed for your field constraints
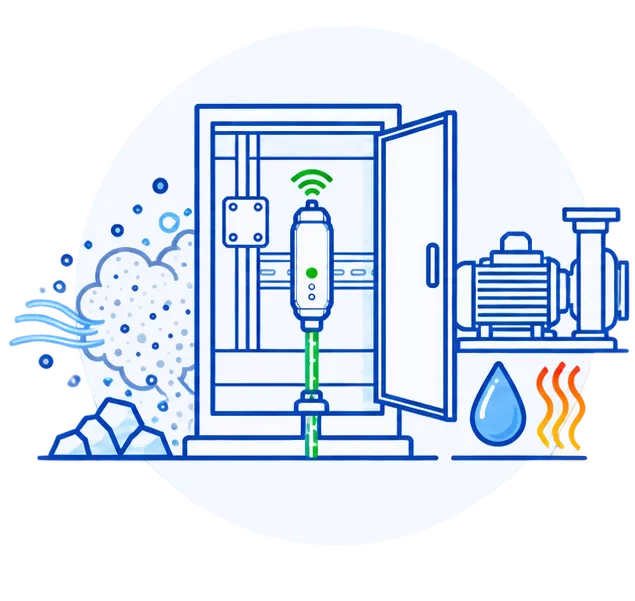
Sensor outside the harsh zone
RED is installed in the electrical cabinet, away from the production area and protected from dust, shocks and other stresses.

A single sensor per machine
A single measurement point to monitor the motor and the driven load, keeping instrumentation to a minimum for a large machine fleet.
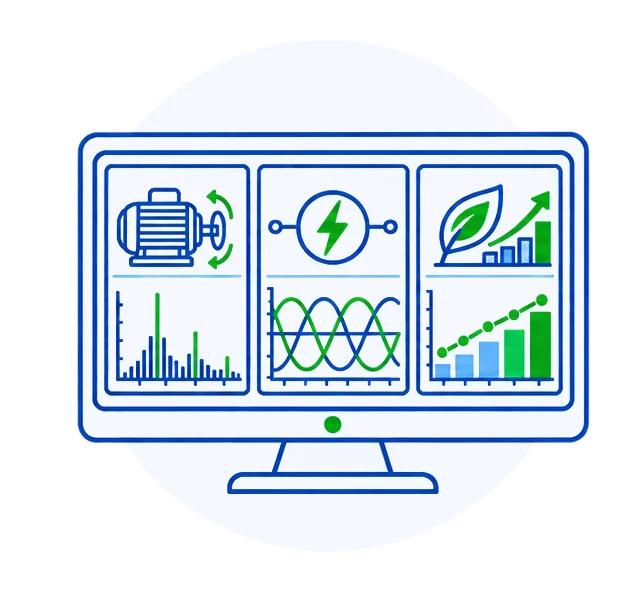
Mechanical, electrical and energy overview
RED combines these 3 types of data to provide a more complete and reliable picture of equipment health and performance.
AT EVERY STAGE OF THE PROCESS
What equipment can you monitor with RED?
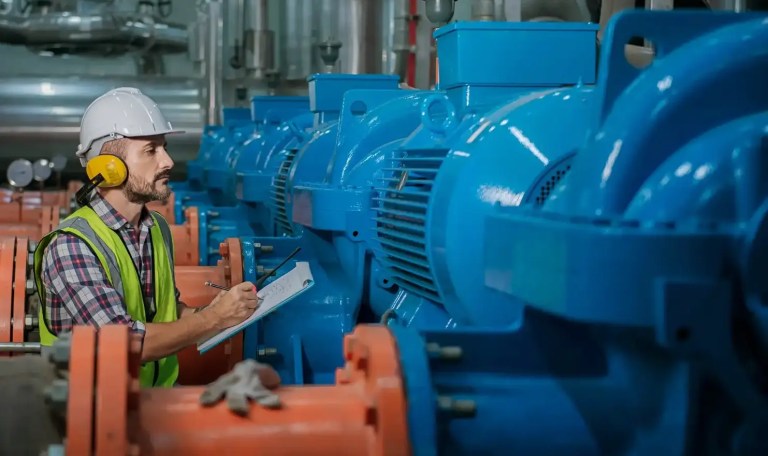
They feed your chemical reactions under pressure, liquefy the gases or distribute the control air for your valves. Far from the risk zones, we detect:
Mechanical unbalance
Problems with anchoring
Deviations in load or hydraulic operation
Lobe damage or wear
Wear of the couplings
Electrical faults and abnormal changes in consumption